- Home
- Extruders and Pelletizers
- Extruder Barrels
Extruder Barrels
Barrel sections, bimetallic liners and complete barrel trains — new manufacture and refurbishment
Barrel sections, bimetallic liners and complete barrel trains — new manufacture and refurbishment
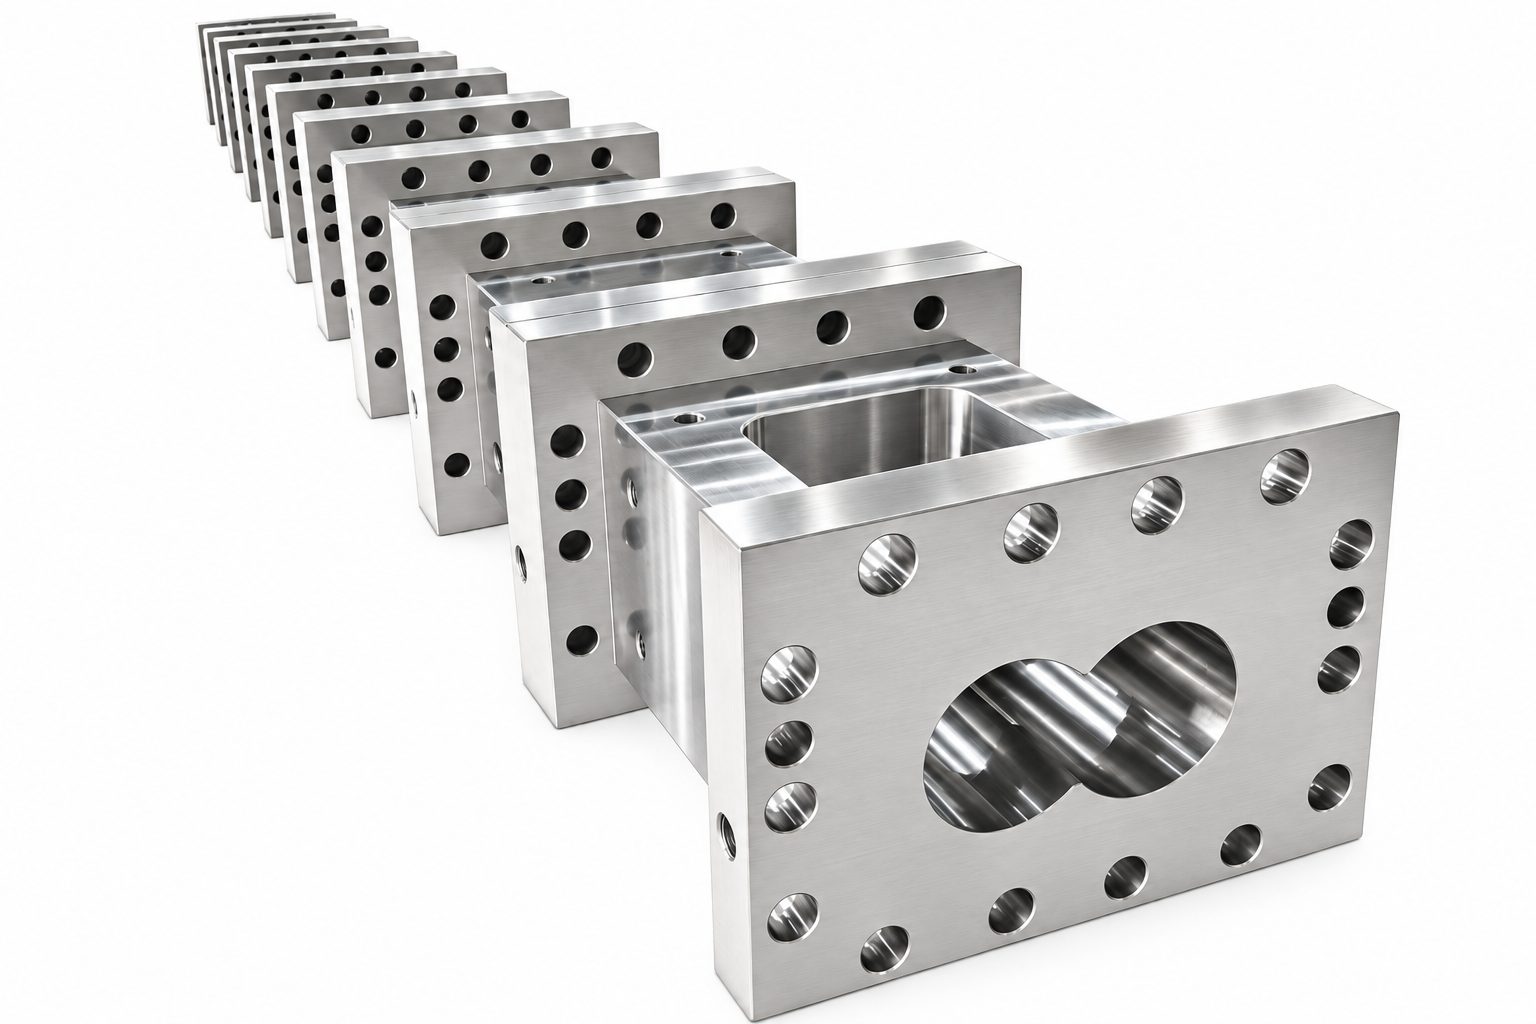
We manufacture new extruder barrels and refurbish worn barrels for every extruder in service: twin-screw co-rotating and counter-rotating compounders, single-screw extruders and extruder-pelletizer lines. We supply individual barrel sections, bimetallic and solid-bore barrels, replacement liners, and complete barrel trains bored, matched and aligned to your machine.
Feed barrels — hopper-throat sections with feed pockets, undercut geometry and intensive cooling.
Vent and side-feed barrels — atmospheric and vacuum vent sections, side-feeder and side-degassing housings.
Closed and conveying barrels — plain closed sections in all standard and custom lengths.
Combi and injection barrels — liquid and additive injection sections with nozzle bosses, valve seats and pressure-tight port fittings.
Bimetallic barrels and liners — centrifugally cast wear-alloy inlays and replaceable sleeves for abrasive and corrosive service.
Discharge and adapter barrels — end sections, transition pieces and die-plate adapters.
Complete barrel trains — a full set bored, honed, matched section to section and shipped ready to install, with heating and cooling provisions in place.
We manufacture and supply new and replacement barrels, barrel sections and liners for all extruder platforms in service today, including — but not limited to — the machines below.
| Manufacturer | Extruder models and families |
|---|---|
| JSW — The Japan Steel Works | CMP251, CMP274, CMP308, CMP335, CMP362, CMP387, CMP443; CIM360, CIM400, CIM460, CIM510, CIM560 |
| Kobelco | LCM, KTX and TSR families; LCM-H, LCM-EX, LCM-G, Hyper KTX, NEX-T, Mixtrumat and NCM legacy families |
| Coperion | ZSK MEGAcompounder family, including ZSK 380 and ZSK 420 |
| ENTEK | HT 162 |
| Farrel Pomini | FCM and FMP systems, including FMP100 |
| KraussMaffei | KE, ZE-PC and ZE BluePower families |
| Leistritz | ZSE 260 MAXX |
| All other makes | Single-screw, co-rotating and counter-rotating twin-screw extruders of any manufacturer, model or age |
Platforms not listed are equally within scope, including obsolete and out-of-production equipment reproduced by reverse engineering. The extruder manufacturer and model are sufficient to open a project.
Our extruder program is built around JSW equipment. We hold established manufacturing experience across the CMP and CIM platforms: bore geometry and center distance, flange and tie-bar interfaces, feed and vent port arrangements, heating and cooling circuit layouts, liner alloy specifications and the wear mechanisms that limit barrel life on these machines.
The following barrel components are supplied for the JSW CMP251, CMP274, CMP308, CMP335, CMP362, CMP387 and CMP443, and for the CIM360, CIM400, CIM460, CIM510 and CIM560:
| Component | Supply |
|---|---|
| Feed barrel | New manufacture and refurbishment |
| Vent barrel | New manufacture and refurbishment |
| Closed barrel | New manufacture and refurbishment |
| Bimetallic liners and sleeves | New manufacture and replacement |
| Complete barrel train | New manufacture and refurbishment |
Barrel sections are supplied individually, as a complete matched train, or within a wider extruder and pelletizer package covering screws and screw elements, die plates, pelletizer knives, mechanical seals, couplings and bearing bushes — including Nordson BKG pelletizer drive and rotor parts — with interface dimensions coordinated across the assembly.
| Application | Materials |
|---|---|
| Barrel body | Nitriding steels (41CrAlMo7-10, 31CrMoV9) and quenched-and-tempered alloy steels (42CrMo4 / 4140, 4340); gas- or plasma-nitrided bore |
| Bimetallic liners | Centrifugally cast iron-based boride alloys for abrasion; nickel-based alloys with tungsten carbide for combined abrasion and corrosion; nickel-chromium-boron alloys for corrosive compounds |
| Solid liners and sleeves | PM HIP tool steels, high-chromium tool steels and corrosion-resistant grades for halogenated, acidic and filled compounds |
Liner alloys are selected against the actual wear mechanism — abrasion, corrosion or both — and upgraded where the original material was under-specified for the process.
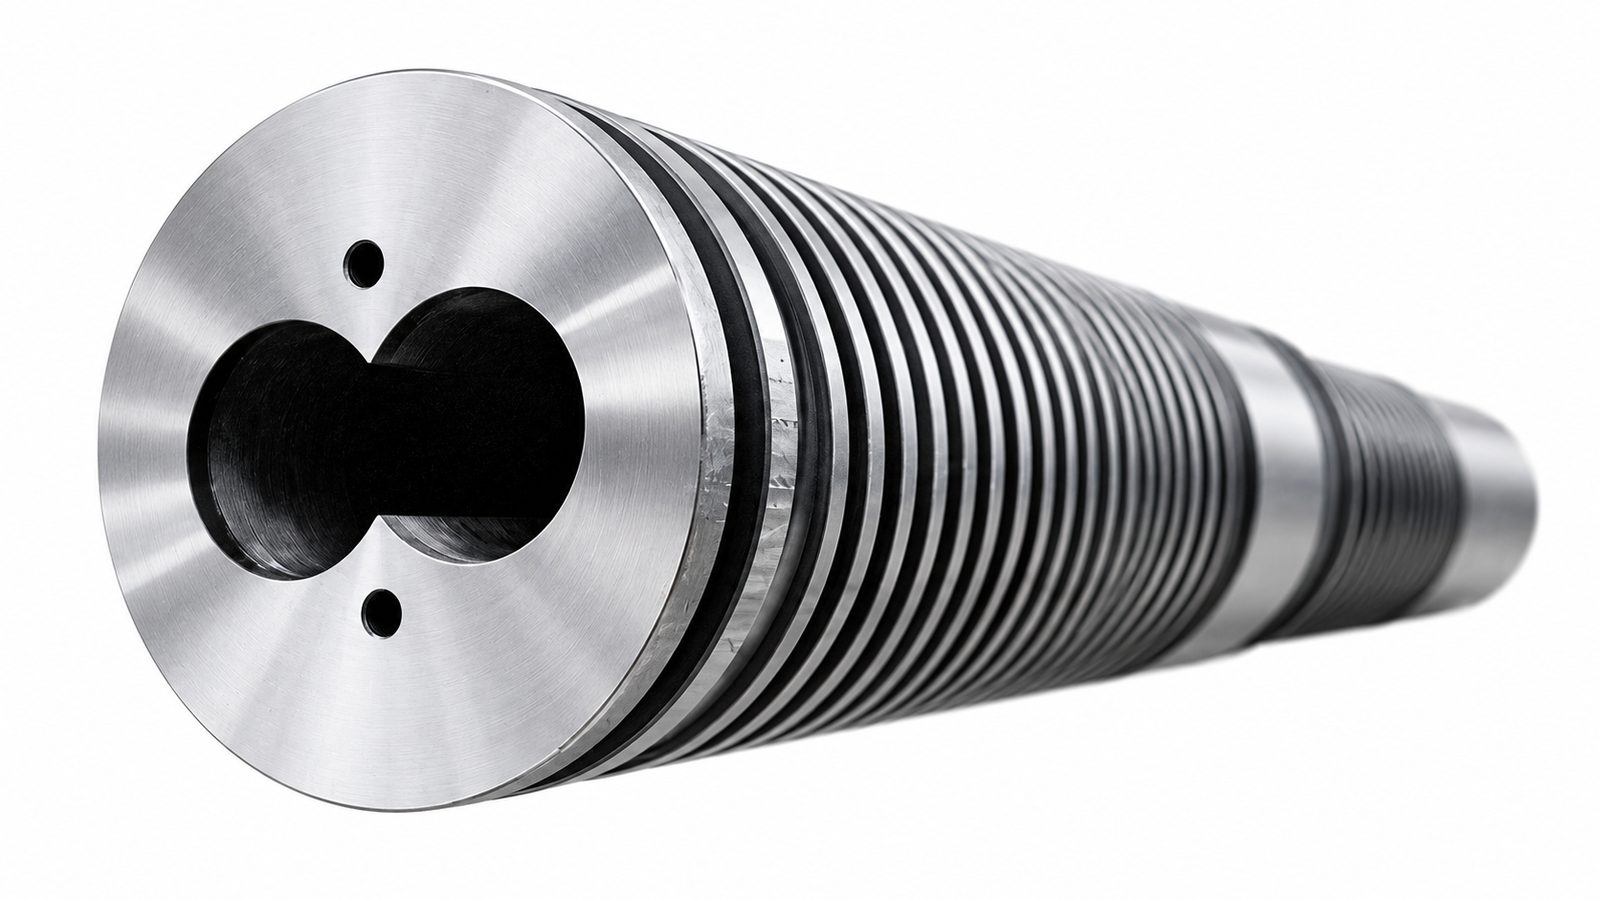
Most worn barrels can be restored to original bore diameter and clearance and returned to service at a fraction of the cost of a new barrel train.
Barrels relined with an upgraded wear alloy routinely outlast the original bore.
We hold the technical information needed to produce barrels for the platforms above. Where a barrel is obsolete, undocumented or from an out-of-production machine, we reverse engineer it from the worn part: full dimensional capture of bore, center distance, ports, flanges and circuits, material and hardness analysis, and a complete manufacturing drawing package that becomes the permanent record for repeat supply.
Every barrel is delivered with material certificates, hardness and dimensional inspection records, bore and center-distance measurement reports, pressure test records for the heating and cooling circuits, and a section-to-section assembly check. Manufacturing is carried out at ISO 9001 certified facilities.
2570 N. First Street, Second Floor, San Jose, CA 95131, USA
Tel. +1-408-892-2364