- Home
- Extruders and Pelletizers
Extruders and Pelletizers
- Capital parts and wear parts
- Refurbishment
- Reverse engineering
- Maintenance services
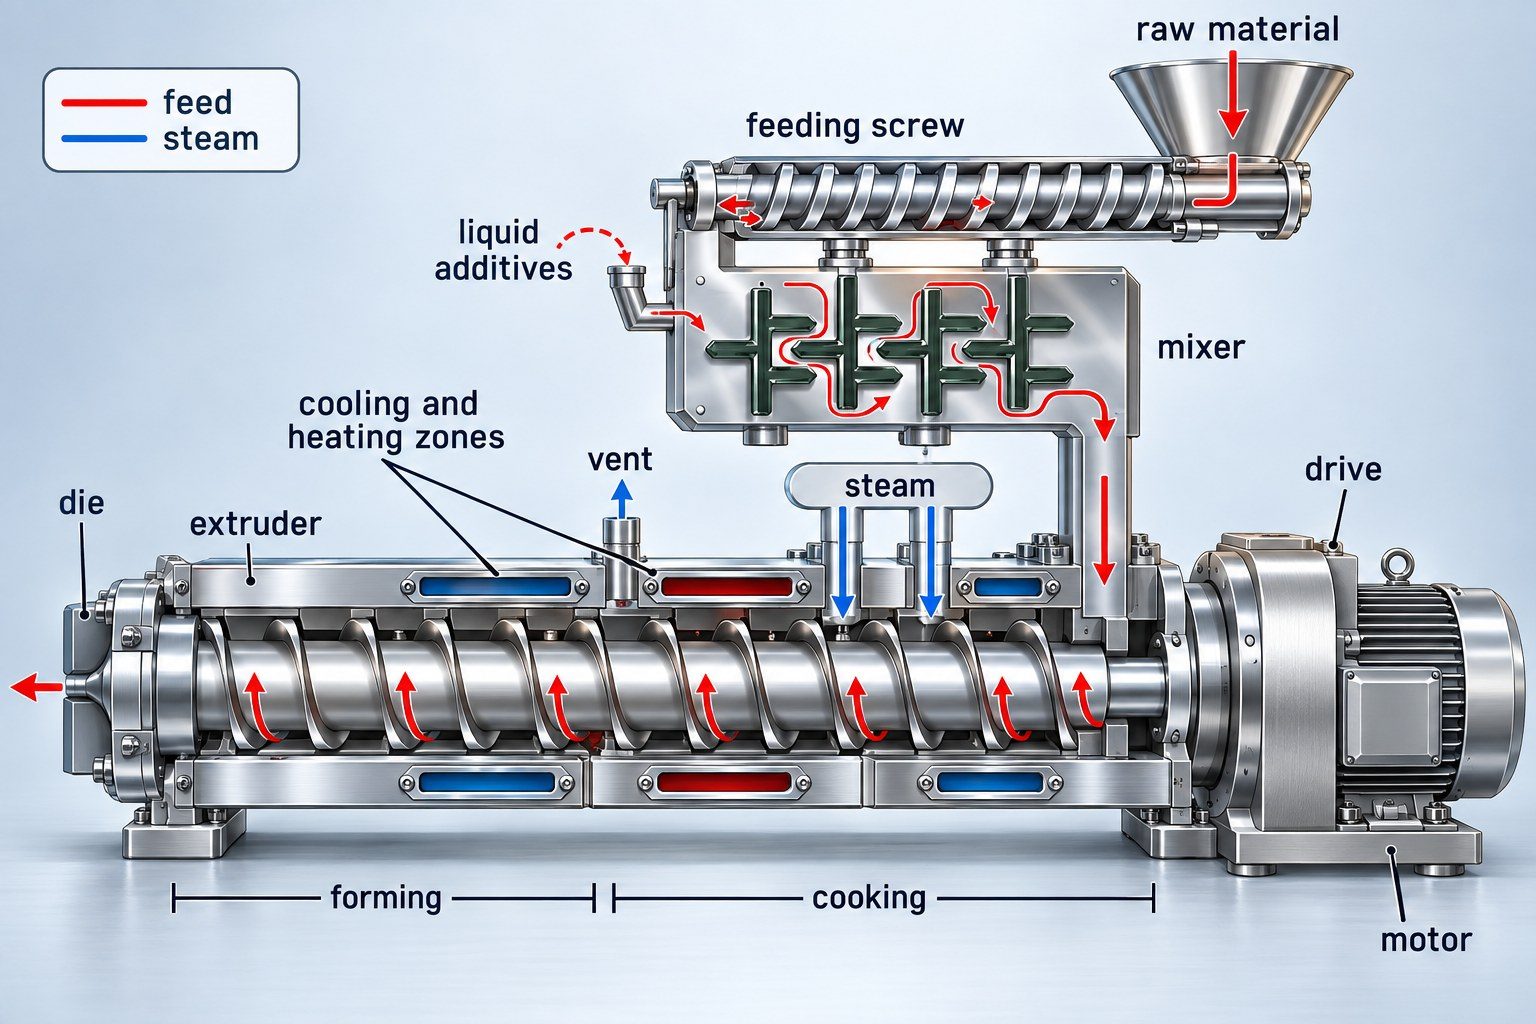
UNEW Industries manufactures, refurbishes and reverse engineers the capital parts of compounding extruders and the pelletizer heads attached to them — shafts, screw elements, barrels, die plates, knives, mechanical seals, couplings and bearing bushes — for every make and model of extruder in service. The extruder and its pelletizer run as one machine, and we supply them as one scope.
We hold our own technical data for every part we make. The extruder manufacturer and model are sufficient to open a project.
| Line | Scope |
|---|---|
| Capital parts | Shafts, screw elements, barrels and liners, die plates, pelletizer knives, mechanical seals, couplings and bearing bushes — new manufacture to UNEW technical data, item by item or as a matched extruder and pelletizer package |
| Wear parts and accessories | Side feeders and stuffers, vent inserts, gearbox and thrust pack parts, heaters and sensors, screen changers, cutter hubs, water boxes, chamber liners and pellet-handling parts |
| Refurbishment | Worn parts restored to original geometry and clearance, with the wear material upgraded where the original was under-specified for the compound |
| Reverse engineering | Parts reproduced from a used sample and our own manufacturing records, and made a UNEW product under a UNEW part number |
| Maintenance services | Strip-down inspection, screw and barrel wear surveys, die and knife matching, turnaround support and technical advice on the line |
| Manufacturer | Extruders and pelletizers |
|---|---|
| JSW — The Japan Steel Works (specialty) | CMP251, CMP274, CMP308, CMP335, CMP362, CMP387, CMP443; CIM360, CIM400, CIM460, CIM510, CIM560, with their ADC pelletizing heads |
| Kobelco | LCM, KTX and TSR families; LCM-H, LCM-EX, LCM-G, Hyper KTX, NEX-T, Mixtrumat and NCM |
| Coperion | ZSK MEGAcompounder family, including ZSK 380 and ZSK 420 |
| Farrel Pomini | FCM and FMP systems, including FMP100 |
| KraussMaffei | KE, ZE-PC and ZE BluePower families |
| ENTEK, Leistritz | HT 162; ZSE 260 MAXX |
| Pelletizing systems | Nordson BKG (including Type AH D drive and rotor parts), Gala, Maag and equivalent underwater, water-ring, hot-face and strand systems |
| All other makes | Single-screw, co-rotating and counter-rotating twin-screw extruders and their pelletizers, of any manufacturer, model or age, including out-of-production machines |
Our extruder program was built around JSW equipment, and the CMP308 is the machine we know best. We hold the complete technical data set for the CMP and CIM platforms: shaft and spline systems, screw element and kneading block geometry, element stacking for PP, HDPE and LLDPE service, barrel bore and centre distance, die and cutting-face arrangements, sealing and bearing interfaces — and, from years of work on these machines in production, the wear and failure mechanisms that actually limit part life on them.
| Part | Location | Supply |
|---|---|---|
| Shafts | Extruder | New manufacture to 800 mm finished diameter and refurbishment; splined and keyed, single-piece and sectional, in matched pairs |
| Screw elements | Extruder | Conveying, kneading, mixing and specialty elements, complete screw sets — new manufacture and refurbishment |
| Barrels and liners | Extruder | Feed, vent, side-feed, combi, closed and discharge barrels, bimetallic liners, complete barrel trains — new manufacture and refurbishment |
| Die plates | Pelletizer head | Underwater, water-ring, hot-face and strand die plates, nozzle inserts, heating and insulation assemblies — new manufacture and refurbishment |
| Pelletizer knives | Pelletizer head | Blades, cutter hubs and blade holders in matched sets — new manufacture and regrind |
| Mechanical seals | Extruder and pelletizer head | Cutter shaft cartridge seals, seal faces, shaft seals, housings and static sealing — new manufacture and refurbishment |
| Couplings | Extruder | Screw-to-gearbox couplings, spline adapters, torque limiters, motor couplings — new manufacture and refurbishment |
| Bearing bushes | Extruder and pelletizer head | Journal bushes, thrust washers, wear rings, steel-backed bimetal bushes — new manufacture to original or fitted size |
Each part has its own page with the full scope of supply, the JSW component table and the refurbishment process.
| Location | Parts |
|---|---|
| Extruder | Side feeders, side stuffers and vent stuffers; vent plugs, inserts and port screens; feed hoppers, throats, liners and grid bars; gearbox torque-distribution gears, thrust bearing packs and shaft seals; tie rods, barrel clamps and flange bolting; heater bands, cartridge heaters, thermocouples and RTDs; cooling manifolds, valves and jackets; melt pressure and temperature sensors, rupture discs; wear plates, spacers and shims |
| Pelletizer head | Discharge adapters, screen changers, breaker plates and screen packs; melt pump wear parts, start-up and diverter valves; cutter hubs, heads, shafts, bearings and blade-pressure mechanisms; water boxes, cutting chambers, chamber liners and wear plates; die-face insulation plates and heaters; spray rings, water housings and pellet water piping; strand pelletizer parts, dryer rotors, blades, screens and classifier panels |
| Part | Materials | For |
|---|---|---|
| Shafts, couplings | Forged alloy and nitriding steels — 42CrMo, 34CrNiMo6 and equivalent — heat treated, nitrided or case hardened on splines | Torque and fatigue duty of the machine |
| Screw elements | Nitriding steel; PM HIP tool steel; NiCr and tungsten carbide hardfaced flight lands; carbide-clad elements | Filled and glass-reinforced PP, abrasive and corrosive compounds |
| Barrels | Nitrided bores; bimetallic centrifugally cast wear-alloy liners; corrosion-resistant alloys | Abrasive and flame-retardant compounds |
| Die plates and knives | Stellite, tungsten carbide and HVOF cutting faces; carbide and ceramic nozzle inserts; D2, M2, 420 and 440C blades, carbide-tipped | Abrasive, filled and glass-reinforced compounds |
| Seals and bushes | Silicon carbide, tungsten carbide and carbon-graphite faces; FKM, FFKM, EPDM and PTFE elastomers; CuSn12 and CuPb10Sn10 bronze, aluminium bronze, steel-backed bimetal | Pellet water quality, temperature, load and lubrication |
Worn capital parts are rarely finished. Most are restored to original geometry and clearance at a fraction of the cost of new — extruder and pelletizer head alike — and parts rebuilt with an upgraded wear material routinely outlast the original.
| Step | Operations |
|---|---|
| 1. Incoming inspection | Dimensions, hardness and crack detection against original geometry — flight and root diameters, bore wear and centre distance, face flatness, spline fit, running clearance |
| 2. Condition report | Measured wear against service limits, remaining life, and the recommendation: rebuild, replace or run on |
| 3. Cleaning | Polymer removal, cooling bore and channel cleaning, pressure test of heating and cooling circuits |
| 4. Rebuild | Flight and crest overlay, barrel reboring and relining, die-face resurfacing and re-nozzling, knife regrind and re-tipping, spline and journal repair, shaft straightening, seal face re-lapping |
| 5. Surface treatment | Re-nitriding, hardfacing or coating; alloy upgrade where the original under-performed |
| 6. Final inspection | Dimensional and hardness verification, matched-set trial assembly, running clearance and die-face-to-knife contact check before shipment |
We hold the technical data for every part we supply. Where a part is not yet in our library, or the machine is out of production, we reverse engineer it from a used sample, from the mating parts, and from our own manufacturing records — and make it a UNEW product.
| Step | Scope |
|---|---|
| Geometry capture | 3D scanning and CMM measurement of the part and its mating features — spline data, flight and lobe profiles, bore and centre distance, nozzle pattern, face and seal geometry, fits and clearances |
| Material analysis | Composition, hardness, case depth and coating of the original; identification of face materials and elastomers |
| Engineering | UNEW drawings, datasheet and process routing; material or surface treatment upgraded where the documented failure mechanism calls for it |
| First article and field validation | Manufacture, inspection and trial assembly; installation on the line and wear surveyed through a full campaign, with results fed back into the design |
From the first order onward the part is manufactured to UNEW data under a UNEW part number, and every repeat order, spare and repair is made to the same data. The plant is no longer dependent on one maker for one machine.
Complete capital-parts scope — twin screw shafts, screw elements, barrels, die plates, knives, bearing bushes, couplings and mechanical seals — reverse engineered and manufactured for a polyolefin producer running four JSW CMP machines (CMP308, CMP335, CMP362 and CMP443) with ADC underwater pelletizers on PP, HDPE and LLDPE; parts validated on the line through full campaigns and now supplied on a life-cycle basis.
Premature screw and barrel wear, die-plate freeze-off and nozzle clogging on a JSW CMP308 solved as one failure chain: PM HIP tool-steel elements with carbide hardfacing, a bimetallic barrel liner and a corrected die thermal package — at least double the previous part life, with freeze-off and clogging eliminated as a recurring failure mode.
Extruder and pelletizer parts supplied to refineries and petrochemical producers in Southeast Asia and beyond, on JSW, Kobelco and other platforms, alongside our gas turbine and compressor work at the same plants.
UNEW Industries operates an ISO 9001 quality management system. Every part carries full material traceability with mill certificates, a dimensional inspection report, hardness, case-depth and coating verification, and a matched-set trial assembly before shipment. Parts are manufactured and refurbished to original design intent and are interchangeable with the original components.
2570 N. First Street, Second Floor, San Jose, CA 95131, USA
Tel. +1-408-892-2364