- Home
- Turbines
- Turbine Repair and Refurbishment
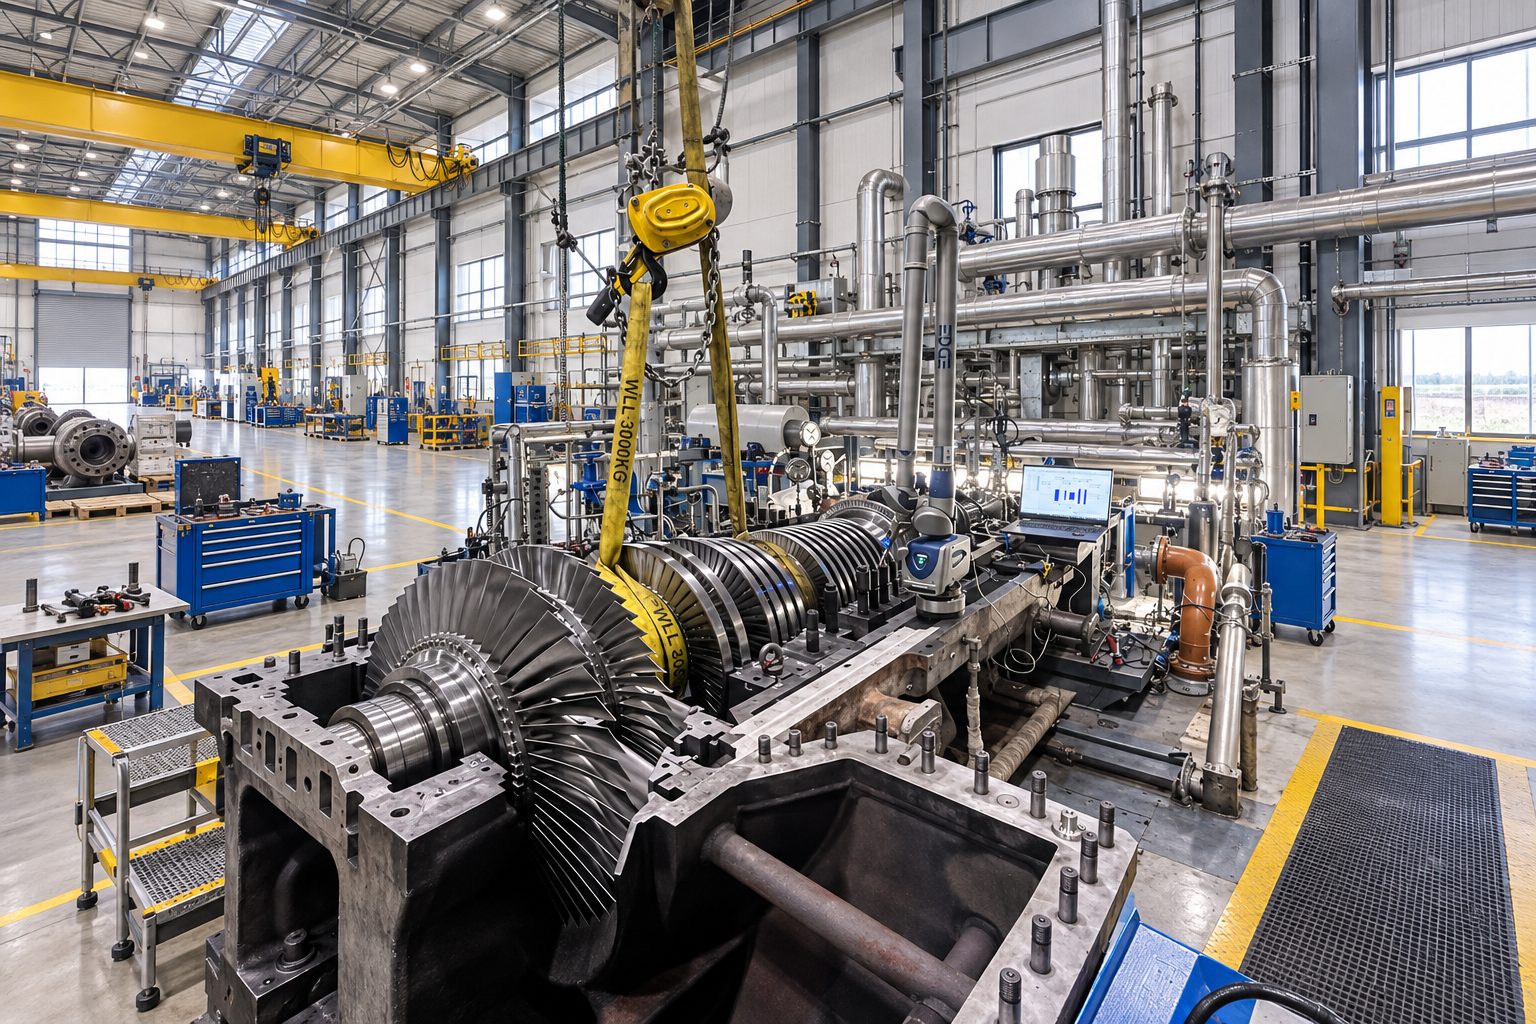
UNEW Industries refurbishes gas turbine and steam turbine components and rotors of any origin — OEM or non-OEM — in one workshop organization, under one set of procedures. The objective is fixed at receipt: return the parts for further roll-in/roll-out cycles at design dimensions, with every repair decision anchored to a measured value and every part returned with its own serialized record.
The processes we apply are the processes of our aviation workshop — robotic thermal spray, vacuum heat treatment, 5-axis laser and EDM machining, high-speed balancing and calibrated flow and frequency benches — applied to heavy-duty turbine parts.
What We Refurbish
| Machine | System | Components |
|---|---|---|
| Gas turbine | Combustion | Combustion caps and liners, transition pieces, fuel nozzles, burner assemblies, cross-fire tubes, flow sleeves |
| Gas turbine | Hot gas path | Turbine buckets / blades rows 1 to 4, turbine nozzles / vanes rows 1 to 4, shroud blocks and ring segments, seal rings |
| Gas turbine | Compressor | Inlet guide vanes, compressor rotor blades and stator vanes, exit guide vanes; complete compressor blading sets in situ or on the rotor |
| Gas turbine | Rotor | Compressor and turbine rotors: journal and seal-area restoration, wheel and dovetail repair, re-blading, balancing |
| Steam turbine | Rotor and blading | HP, IP and LP rotors: journal and coupling restoration, shaft straightening, wheel and dovetail repair, partial or complete re-blading, shroud and tenon work, balancing and overspeed |
| Steam turbine | Stationary steam path | Diaphragms, nozzle blocks, blade carriers, inner casings and shroud rings: crack repair, profile restoration, seal-land hardfacing, re-blading of welded diaphragms |
| Steam turbine | Seals, bearings, valves | Gland and interstage seals, journal and thrust bearings (re-babbitting), stop, control and intercept valve internals (seat and disc restoration, stem repair, hardfacing) |
Workshop Areas
The workshop covers 500,000 square feet (46,000 m²) and is organized as a single flow from receipt to release. Each area has its own equipment, procedures and records, and a part moves through the areas its repair routing calls for.
| Area | Function and key equipment |
|---|---|
| Receiving and incoming inspection | Serial registration, photographic record, visual and dimensional survey; 3D optical scanners, coordinate measuring machines, portable measuring arms, rotor runout stands |
| Cleaning and stripping | Chemical coating removal, thermal barrier removal, grit and glass-bead blasting, ultrasonic and high-pressure water cleaning, fluoride ion cleaning of superalloy cooling passages |
| Non-destructive testing | Fluorescent penetrant lines, magnetic particle benches, phased-array and conventional ultrasonic, eddy current, digital radiography, borescope and videoscope |
| Metallurgical laboratory | Optical emission spectrometry, metallographic sectioning and microscopy, hardness testing, coating thickness and bond evaluation, failure analysis |
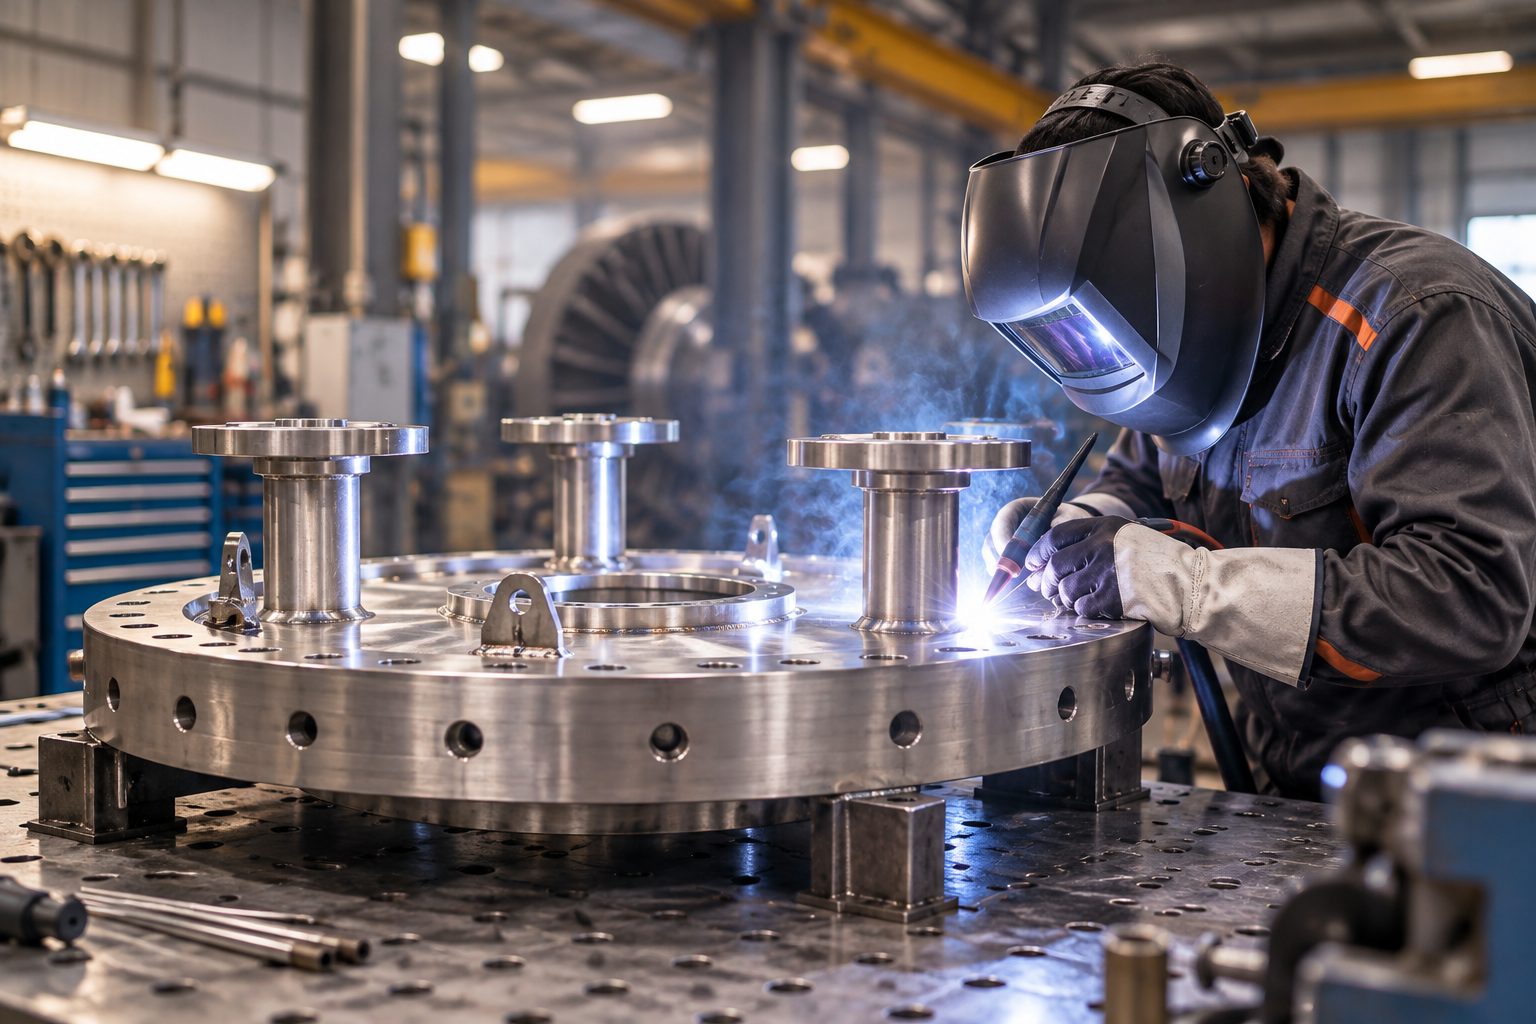
| Welding and cladding | Micro-TIG and TIG stations, electron-beam welding, laser cladding, plasma transferred arc, automated tip-restoration welding, submerged-arc for rotor journal build-up, dedicated superalloy welding cells with pre-heat |
| Heat treatment and brazing | Vacuum furnaces for solution, precipitation, diffusion and stress-relief cycles; vacuum brazing; hot isostatic press; internal vapor-phase aluminide furnace |
| Coating | Robotic HVOF and APS booths, vacuum plasma spray, coating masking and stripping, witness-coupon laboratory |
| Cooling-hole machining and flow | 5-axis laser drilling, 5-axis and multi-head EDM, shaped-hole capability, calibrated cooling-flow benches |
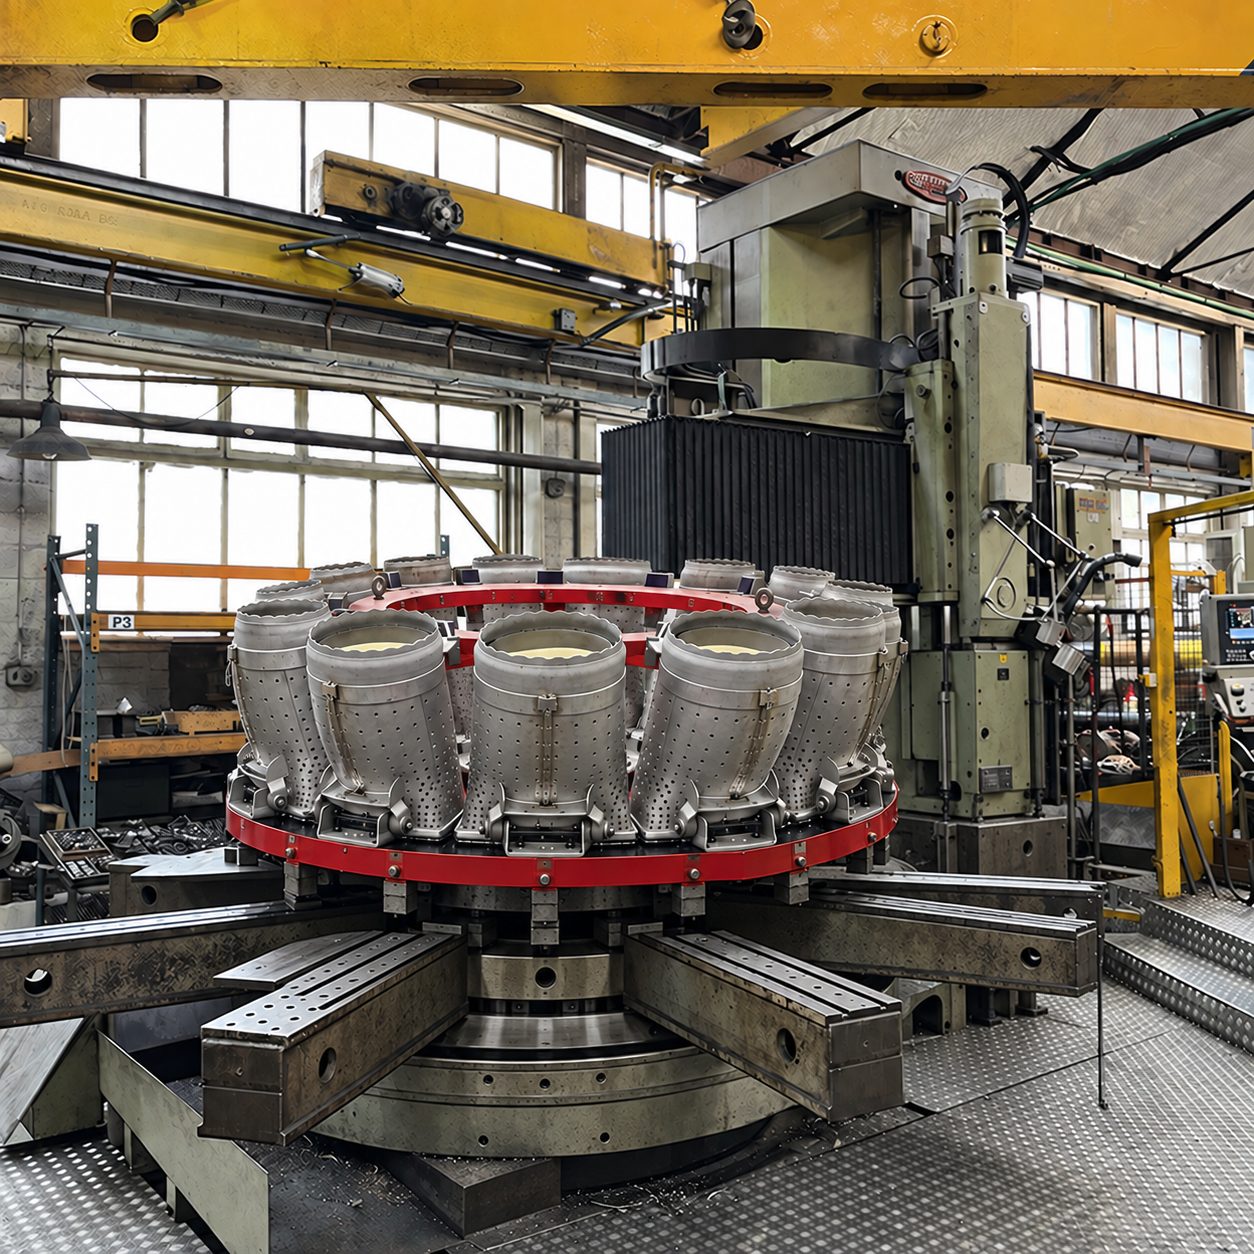
| Machining | 5-axis machining centers, creep-feed grinders, vertical boring and turning mills for combustion hardware, casings and rings, rotor lathes, wire and sinker EDM |
| Blade tuning and rotor balancing | Natural-frequency and moment-weight benches, low-speed balancing machines, high-speed balancing and overspeed facility for complete rotors |
| Assembly, final inspection and release | Set assembly and distribution, final dimensional and NDE inspection, report compilation, protective packaging and rotor shipping cradles |
Equipment and Technologies
| Technology | What it does for the part |
|---|---|
| 3D optical scanning and CMM | Captures the complete geometry of the part at receipt and at release; every dimension is compared against the engineered drawing, not against a worn reference. Portable measuring arms take the same measurement on rotors and casings too large for the CMM table |
| Fluoride ion cleaning | Removes oxides from cracks and cooling passages in nickel- and cobalt-base superalloys so that weld and braze repairs bond to clean parent metal |
| Micro-TIG and automated welding | Restores tip shrouds, squealer tips, Z-notches, platform edges and seal lands with controlled heat input; automated cells give the same bead on every part of the set |
| Electron-beam and laser welding | Joins and repairs thin combustion hardware and cover plates with minimal distortion |
| Laser cladding | Rebuilds wear surfaces — seal lands, contact faces, valve seats, journals — with a metallurgically bonded overlay in a hardfacing or base-matching alloy |
| Vacuum heat treatment and HIP | Rejuvenates creep-damaged superalloy microstructure, closes internal porosity and restores the properties of the base alloy before recoating |
| Robotic HVOF, APS and VPS coating | Applies MCrAlY bond coats and 7YSZ thermal barrier coatings, including dense vertically cracked TBC on rows 1 and 2, with the same thickness distribution on every airfoil |
| Vapor-phase aluminide | Coats the internal cooling passages of buckets and nozzles against oxidation where no line-of-sight process can reach |
| 5-axis laser and EDM cooling-hole restoration | Reopens and re-drills film-cooling and effusion holes closed by coating or weld repair, at the design angle and diameter, including shaped holes |
| Calibrated cooling-flow benches | Verifies the cooling air flow of every cooled part against the design value before it is released — the single most important check for hot gas path life |
| Natural-frequency and moment-weight benches | Verifies that every refurbished or replacement blade sits in the design frequency band and moment-weight class, and records the set distribution |
| Vertical boring and turning mills | Machine combustion liners, transition-piece frames, casings, rings and shroud blocks in fixtures that hold a complete set to a common datum |
| High-speed balancing and overspeed | Balances complete gas turbine and steam turbine rotors at operating speed and proves them to trip speed before return |
| Metallurgical laboratory | Confirms base-alloy condition by sectioning a coupon, identifies the cause of premature damage, and fixes the repair level from evidence rather than appearance |
Refurbishment Process
Every set follows the same sequence. The incoming inspection report fixes the repair level of each part — light, medium or heavy — against measured values, and identifies before any work begins the parts that are not economical to repair.
| Step | Operations |
|---|---|
| 1. Receipt and incoming inspection | Serial registration, photographic record, visual, dimensional and NDE survey, coating and wall-thickness measurement, metallurgical coupon where the base alloy is in question; repair classification per part |
| 2. Strip and clean | Coating and thermal barrier removal, blast cleaning, fluoride ion cleaning of cooling passages; de-blading of affected steam turbine rows, removal of shrouds and locking hardware |
| 3. Repair | Weld build-up, crack repair, braze, section and tip replacement, cooling-hole restoration; rotor journal and dovetail repair, shaft straightening, re-blading, shroud and tenon work, diaphragm repair, valve seat and disc restoration |
| 4. Heat treatment | Solution and rejuvenation heat treatment, hot isostatic pressing, post-weld stress relief |
| 5. Recoat and surface treatment | Bond coat, thermal barrier and internal aluminide on gas turbine parts; erosion shields, hardfacing and diffusion treatments on steam turbine parts |
| 6. Balance, inspect and release | Dimensional and NDE inspection, cooling-flow verification, blade frequency and moment weighing, low- and high-speed balancing and overspeed of rotors; serialized final refurbishment report and certificate of conformance |
Aviation-Standard Restoration
Standard refurbishment returns a part to serviceable condition for the next interval. Aviation-standard restoration goes further: HIP rejuvenation of the base alloy, DVC thermal barrier coating, internal aluminide, cooling-hole restoration to the design pattern and a verified cooling flow on every cooled part, with wear parts replaced in higher-grade material than the original. The result is a part that runs longer than it did when new, and a set that returns for additional roll-in/roll-out cycles with less heavy repair at each one.
Reverse Engineering in Refurbishment
Every part we refurbish is inspected against its engineered drawing. Where a part enters our workshop for the first time, its geometry, material and coating are captured during incoming inspection and the part is added to our library. From then on, a damaged blade, nozzle or liner in that set can be replaced new by a UNEW part that fits the set already in the machine — one component, not a full set.
Reports and Documentation
Each row or component set is returned with a final refurbishment report — per-part serial record, incoming findings, repair level, operations performed, measurements, coating and cooling-flow record, balancing and overspeed record for rotors — and a refurbishment acceptance letter for the complete scope. Repair levels and work volume are stated in the report task by task, so the report and the invoice show the same figures.
Logistics
We collect the parts from the customer's warehouse or from the outage site, pack them in protective fixtures and rotor cradles, and return them by air or sea to the plant. For fleets under a long-term service agreement, a spare set from UNEW inventory can be installed while the customer's set is in our workshop.