- Home
- Gas Turbines
Gas Turbines
- Capital parts, consumables and operational spares
- Repair and refurbishment
- Outage and maintenance services
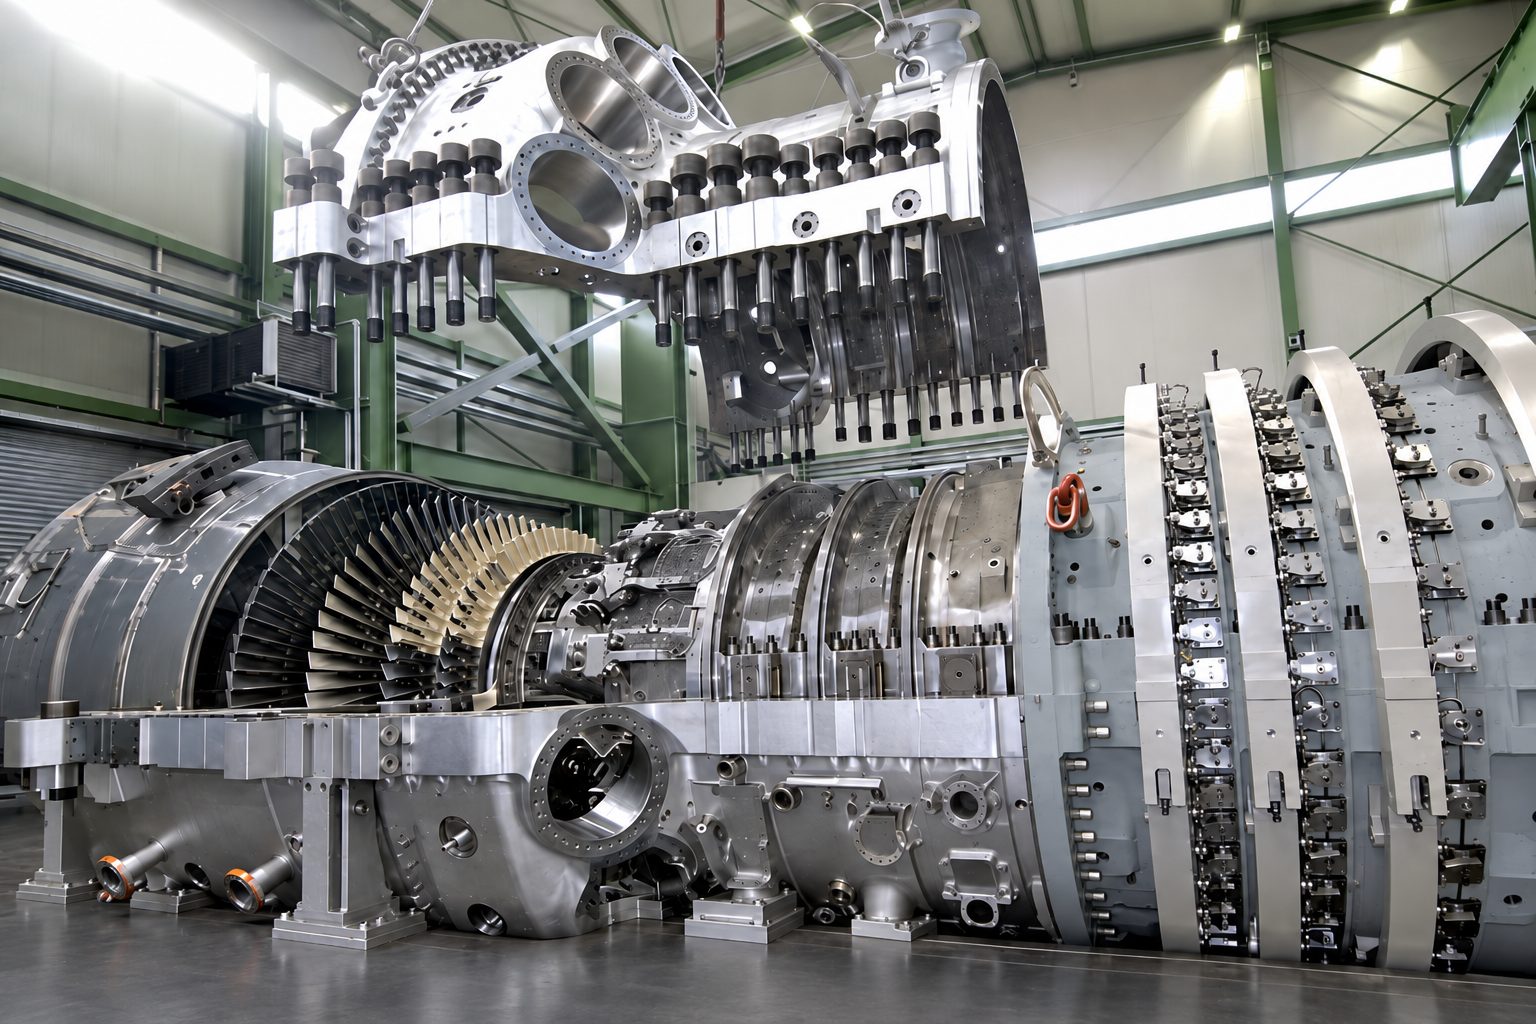
UNEW Industries manufactures, repairs and services the components of heavy-duty gas turbines. We supply the full range of parts a turbine consumes over its life — from complete hot gas path sets to the gaskets and sensors replaced at every inspection — we refurbish the parts that come out, and we run the outages in which they are exchanged.
Our parts are manufactured to aviation standards and meet or exceed OEM specification. We work under long-term service agreements with power producers, refineries and oil and gas operators in Southeast Asia, the Middle East, North Africa and South America.
| Line | Scope |
|---|---|
| Parts supply | Capital parts, consumables and operational spares — new manufacture from our own technical data, delivered with full documentation. |
| Repair and refurbishment | Combustion, hot gas path and compressor components of any origin, restored to aviation standard and returned for further roll-in/roll-out cycles. |
| Maintenance and outage services | Combustion, hot gas path and major inspections; field engineering; borescope; control system and monitoring services; long-term service agreements. |
We supply parts and services for the GE, Siemens, Mitsubishi and Solar fleets listed below, including the ABB / Alstom heritage frames now serviced under GE. Upgrade designations (MXL2, MC2, XL/XP, 7F.04-200 and others) are covered on the base platform.
| Manufacturer | Class | Models |
|---|---|---|
| GE | Heavy-duty | 6B; 6F.01, 6F.03 (6FA); 7B, 7E, 7EA, 7E.03; 7FA.01, 7FA.02, 7FA.03, 7F.04, 7F.05; 7HA.02, 7HA.03; 9E.03, 9E.04; 9FA.01, 9FA.02, 9F.03, 9F.04, 9F.05; 9FB.01, 9FB.02, 9FB.03 |
| GE (ABB / Alstom heritage) | Heavy-duty | GT8, GT8B, GT8C, GT8C2; GT9; GT11D, GT11N, GT11N2; GT13D, GT13E1, GT13E2 — including the DM, DC+, DXC, N2 M, NM/NMC XL/XP, MC2, MXL and MXL2 upgrade configurations |
| GE | Aeroderivative | LM2500, LM2500+, LM2500+G4, LM2500XPRESS; LM6000, LM6000PC, LM6000VELOX; LMS100; TM2500 |
| Siemens | Heavy-duty | SGT5-2000E (V94.2), SGT5-4000F (V94.3A), SGT5-8000H, SGT5-9000HL; SGT6-2000E (V84.2), SGT6-5000F (W501F), SGT6-8000H, SGT6-9000HL; SGT-1000F (V64.3A), SGT5-3000E (V94.2A), SGT6-3000E (W501D5A), SGT6-4000F (V84.3A), SGT6-6000G (W501G), W501D5, V84.3, W251, W191 |
| Siemens | Industrial | SGT-50, SGT-100, SGT-200, SGT-300, SGT-400, SGT-500, SGT-600, SGT-700, SGT-750, SGT-800 |
| Siemens | Aeroderivative | SGT-A05, SGT-A35, SGT-A65 |
| Mitsubishi | Heavy-duty | M701D, M701DA; M501F, M701F, M701F4; M501G, M501GAC, M701G; M501J, M501JAC, M701J, M701JAC |
| Mitsubishi | Industrial / aeroderivative | H-25, H-100; FT8 MOBILEPAC, FT4000 SWIFTPAC |
| Solar Turbines | Industrial | Saturn 20; Centaur 40, Centaur 50; Mercury 50; Taurus 60, Taurus 70; Mars 90, Mars 100; Titan 130, Titan 250, Titan 350 |
| All other makes | Quoted on request |
We manufacture the complete capital parts scope of the gas turbine — every component that is rolled out at a combustion inspection, hot gas path inspection or major inspection.
| System | Components |
|---|---|
| Combustion | Combustion caps and liners, transition pieces, fuel nozzles, burner assemblies, burner inserts and swirlers, cross-fire tubes, flow sleeves |
| Hot gas path | Turbine buckets / blades rows 1–4, turbine nozzles / vanes rows 1–4, shroud blocks and ring segments, seal rings, retaining rings |
| Compressor | Inlet guide vanes, compressor rotor blades — all stages, compressor stator vanes — all stages |
| Rotor | Complete gas turbine rotors (compressor and turbine disc stack), quoted on request |
Parts are supplied as complete sets or as individual items, serialized, under UNEW part numbers cross-referenced to the OEM part number, and delivered with certificate of conformance, material certificate, dimensional record, NDE record and coating record. We maintain a minimum of one spare set in inventory for every model we support.
Every inspection consumes a defined kit of parts. We supply complete inspection kits or individual items: spiral-wound and metallic gaskets, cloth seals, hula seals and seal strips, bolting and locking hardware, shims, cross-fire tube retainers, spark plugs and flame detectors, insulation and lagging, and the hardware consumed at each combustion, hot gas path and major inspection.
The parts that keep the unit running between inspections: thermocouples and RTDs, LVDTs, servo valves, pressure and vibration transmitters, fuel, lube oil and inlet filters, ignition components, and control system cards and I/O modules. As part of our control system services we record every card in the unit — part number, revision, serial number and firmware — so the correct spare is identified before it is needed.
We hold the technical data for every part we supply. Parts not yet in our library are reverse engineered from a used sample (see Reverse Engineering below). From the first order onward the part is a UNEW product with a UNEW part number, and repeat orders are manufactured to the same data.
Because the data is ours, we manufacture only what is required. Operators are not obliged to buy a full set to replace a single failed component.
| Component | Base alloy | Coating system |
|---|---|---|
| Turbine vanes / nozzles | FSX-414 cobalt-base, IN939 and equivalent | MCrAlY bond coat with thermal barrier coating; internal aluminide |
| Turbine blades / buckets | IN738LC, GTD-111 and equivalent nickel-base superalloys | MCrAlY bond coat with thermal barrier coating; internal vapor-phase aluminide |
| Shroud blocks / ring segments | SS310 body with IN738 inner plates; nickel-base alloys | Thermal barrier and abradable systems |
| Combustion liners, transition pieces | Hastelloy X, Nimonic 263 and equivalent | Thermal barrier coating |
| Compressor blades and vanes | Ti-6Al-4V (front stages); X20Cr13 and X22CrMoV12-1 12% chromium steels (rear stages) | Uncoated or erosion-resistant coating to specification |
Coatings are applied on robotic HVOF and APS equipment: VPS/HVOF MCrAlY bond coats, DVC 7YSZ thermal barrier coatings and internal vapor-phase aluminide. Cooling holes are drilled and restored on 5-axis laser and EDM equipment and verified on a calibrated cooling-flow bench.
Reverse engineering is how we bring a new part into production — for any gas turbine make and model, whether or not it appears in the fleet list above. We work from a used part: a component removed at an inspection is all we need. The result is a complete technical package held by UNEW Industries — drawings, material specification, coating specification, process routing and inspection plan — from which the part is manufactured as a UNEW product.
| Step | What we do |
|---|---|
| 1. Sample | A used part is collected from the customer's store or from the parts removed at an outage; the sample is returned after engineering |
| 2. Dimensional capture | 3D optical scanning and CMM measurement of the complete part, including internal cooling passages, cooling-hole pattern and sealing features; measured wear is corrected back to the design condition |
| 3. Material and coating analysis | Chemical composition, hardness, microstructure and heat-treatment condition of the base alloy; identification and thickness of bond coat, thermal barrier and internal coatings |
| 4. Engineering | Manufacturing drawings, material and coating specifications, casting or forging definition, machining and process routing, inspection plan and acceptance criteria |
| 5. First article | Manufacture and full first-article inspection against the engineered data; cooling-flow verification for cooled airfoils; frequency and moment weighing for blades |
| 6. Release | UNEW part number assigned; the part enters our library and is manufactured to the same data on every repeat order |
Reverse engineering is also what makes single-component replacement possible. OEM parts are dimensioned so that they cannot be interchanged with other suppliers' parts; once we hold the exact geometry, we manufacture the one broken component to fit the set already in the machine, rather than replacing the set.
The same data is applied in refurbishment. A repaired part is restored and inspected against its engineered drawing, not against a worn reference, so every dimension returned is a design dimension.
We refurbish combustion, hot gas path and compressor components of any origin — OEM or non-OEM. The objective is set at receipt: return the set for further roll-in/roll-out cycles at the lowest life-cycle cost.
Every set begins with a documented incoming inspection: visual, dimensional, fluorescent penetrant and eddy current examination, coating and wall thickness measurement, and metallurgical sectioning of a coupon where the condition of the base alloy is in question. The report classifies each part as light, medium or heavy repair, with every classification anchored to measured values, and identifies before any work begins the parts that are not economical to repair.
| Step | Operations |
|---|---|
| 1. Receipt and inspection | Serial record, incoming inspection report, repair classification per part |
| 2. Strip and clean | Chemical stripping of coatings, grit blast, thermal barrier removal, cleaning of internal cooling passages |
| 3. Repair | Weld build-up, crack repair, braze, section and tip replacement, dimensional restoration, machining to drawing, cooling-hole restoration by 5-axis laser / EDM |
| 4. Heat treatment | Solution and rejuvenation heat treatment; hot isostatic pressing where required |
| 5. Recoat | Robotic HVOF / APS MCrAlY bond coat, thermal barrier coating, internal vapor-phase aluminide |
| 6. Final inspection and release | Dimensional and NDE inspection, cooling-flow verification, moment weighing of blades, serialized final refurbishment report and certificate of conformance |
Each row or component set is returned with a final refurbishment report — per-part serial record, repair level, measurements and coating record — and a refurbishment acceptance letter for the complete scope.
The processes we apply to gas turbine parts are the processes of our aviation workshop: robotic HVOF and APS coating, internal aluminide furnaces, 5-axis laser and EDM cooling-hole machining and calibrated cooling-flow benches. Wear parts replaced during repair are replaced with higher-grade material than the original. The result is a part that runs longer than it did when new.
| Service | Scope |
|---|---|
| Planned inspections | Combustion inspection (CI), hot gas path inspection (HGPI) and major inspection (MI): planning, parts, tooling, site crew, execution, testing and acceptance |
| Field engineering | Technical field advisors, shift managers, supervisors, mechanical technicians, welders, electricians and riggers |
| Borescope inspection | Pre-outage and interval borescope inspections with report and check sheets |
| Control systems | Health audits of GE Mark VIe and other control systems — hardware record, I/O, software and configuration, HMI and network, alarms and protection, spares — and resolution of control faults |
| Performance | Load testing, wheel-space temperature and cooling-flow investigation, post-outage commissioning |
| Remote monitoring and diagnostics | Remote condition monitoring and diagnosis of the unit between inspections |
| Root cause investigation | Instrumentation faults, premature part deterioration, material and fuel effects on part life |
| Long-term service agreements | Multi-year agreements covering parts, refurbishment, outages and engineering support, with annual maintenance plans, fixed lead times and inventory sets held for the client |
Long-term service agreements on Siemens V94.2 fleets in Egypt, Argentina and the United Arab Emirates — hot gas path inspections, capital parts and refurbishment across compressor, combustion and turbine sections.
GE 6FA units in Vietnam since 2017 — combustion and hot gas path parts, refurbishment, hot gas path inspection outages and control system audits under a long-term service agreement; accepted alongside the OEM by Vietnam's power and refinery operators.
Complete compressor blading sets, rows 1–16, in service since 2018, with more than 60,000 equivalent operating hours accumulated on the longest-running set.
Refurbishment programs of more than 2,000 serialized components per engine, with turbine vanes and blades returned to service through successive 33,000 EOH intervals.
UNEW Industries operates an ISO 9001 quality management system. Gas turbine parts are manufactured, repaired and coated to aviation standards, and every part is traceable by serial number from raw material to delivery. Each delivery carries a certificate of conformance, material certificate, dimensional record, NDE record and coating record.
2570 N. First Street, Second Floor, San Jose, CA 95131, USA
Tel. +1-408-892-2364