- Home
- Extruders and Pelletizers
- Pelletizer Die Plates
Pelletizer Die Plates
Die plates, nozzle inserts and cutting faces — new manufacture and refurbishment
Die plates, nozzle inserts and cutting faces — new manufacture and refurbishment
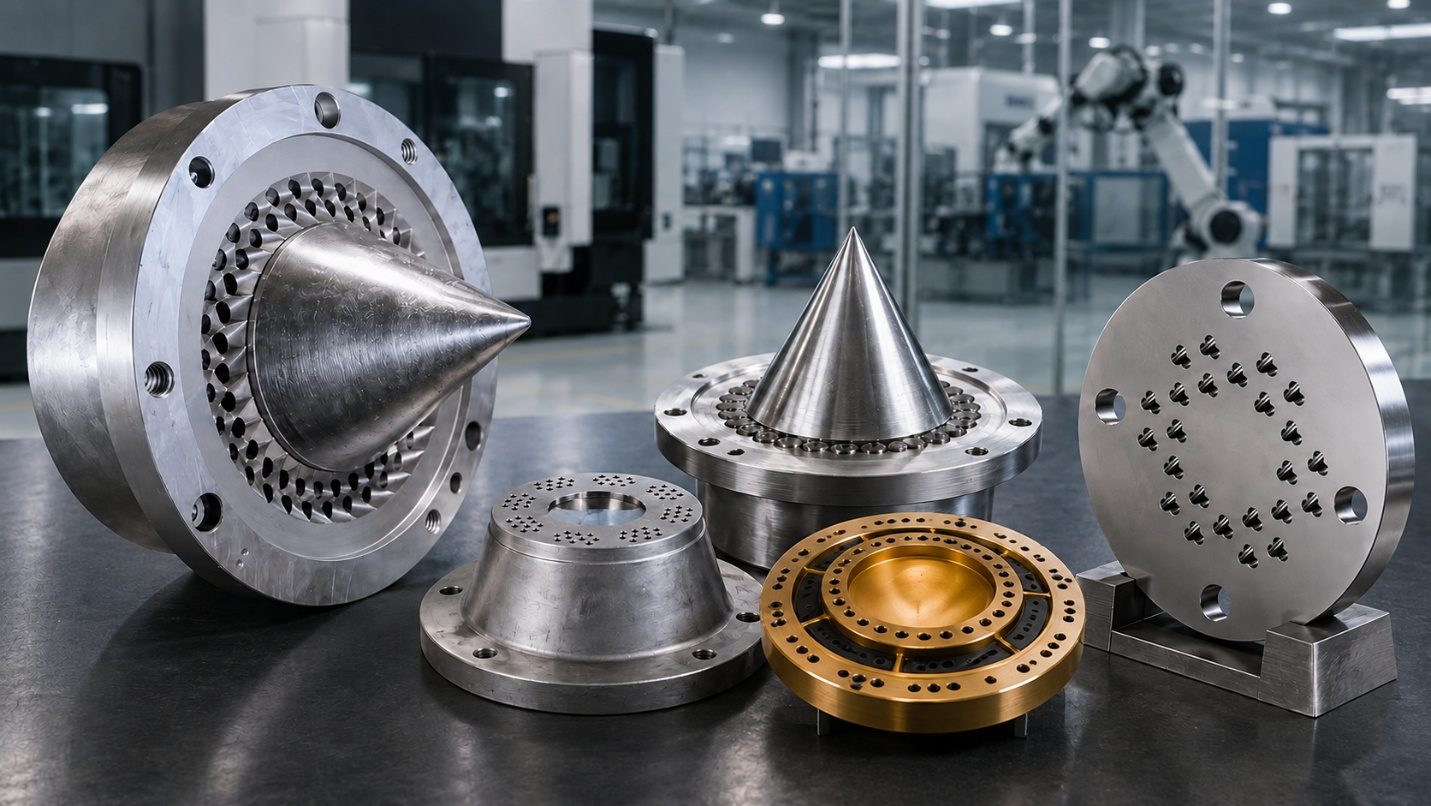
We manufacture new die plates and refurbish worn die plates for the pelletizer heads attached to extruders of every type: underwater, water-ring, hot-face and strand pelletizing. We supply bare plates, fully heated and insulated die assemblies, nozzle inserts and hardfaced cutting faces, machined to your pellet size, throughput and cutter geometry.
Underwater die plates — heated and thermally insulated plates with drilled or insert nozzle patterns, hardfaced or carbide-inserted cutting faces, bored to your pellet size and hole count.
Water-ring and hot-face die plates — die-face cutting plates with matched knife contact surfaces for water-ring, air-cooled and hot-face systems.
Strand dies — strand die heads and plates with single and multiple nozzle rows, heater bosses and melt distribution channels.
Nozzle inserts and bushings — tungsten carbide, ceramic and hardened steel inserts, replaceable individually, with land length and entry geometry set to the compound.
Cutting-face hardfacing — Stellite, tungsten carbide and HVOF-applied faces for abrasive, filled and glass-reinforced compounds.
Heating and insulation assemblies — cartridge, steam and oil-heated die bodies, thermal insulation plates, heater cartridges, thermocouples and pressure-tight fittings.
Adapters and transition pieces — die-plate adapters, discharge and transition pieces matched to the extruder discharge flange and to the cutting chamber.
Matched die and knife sets — die plate, cutter hub and knives supplied together and matched to cutting angle, blade contact and blade pressure.
We manufacture and supply new and replacement die plates, nozzle inserts and cutting faces for all extruder and pelletizer platforms in service today, including — but not limited to — the machines below.
| Manufacturer | Extruder and pelletizer models and families |
|---|---|
| JSW — The Japan Steel Works | CMP251, CMP274, CMP308, CMP335, CMP362, CMP387, CMP443; CIM360, CIM400, CIM460, CIM510, CIM560 |
| Kobelco | LCM, KTX and TSR families; LCM-H, LCM-EX, LCM-G, Hyper KTX, NEX-T, Mixtrumat and NCM legacy families |
| Coperion | ZSK MEGAcompounder family, including ZSK 380 and ZSK 420 |
| ENTEK | HT 162 |
| Farrel Pomini | FCM and FMP systems, including FMP100 |
| KraussMaffei | KE, ZE-PC and ZE BluePower families |
| Leistritz | ZSE 260 MAXX |
| Pelletizing systems | Nordson BKG, including Type AH D drive and rotor parts; Gala, Maag and equivalent underwater, water-ring and strand pelletizing systems |
| All other makes | Die plates for the pelletizer heads of single-screw, co-rotating and counter-rotating twin-screw extruders of any manufacturer, model or age |
Platforms not listed are equally within scope, including obsolete and out-of-production equipment reproduced by reverse engineering. The extruder manufacturer and model are sufficient to open a project.
Our extruder program is built around JSW equipment. We hold established manufacturing experience across the CMP and CIM platforms: nozzle pattern and hole count, bore and land geometry, cutting-face flatness and hardfacing specification, die body heating and insulation layout, adapter and cutting-chamber interfaces, and the wear mechanisms that limit die plate life on these machines.
The following die plate components are supplied for the JSW CMP251, CMP274, CMP308, CMP335, CMP362, CMP387 and CMP443, and for the CIM360, CIM400, CIM460, CIM510 and CIM560:
| Component | Supply |
|---|---|
| Die plate — underwater | New manufacture and refurbishment |
| Die plate — water-ring, hot-face and strand | New manufacture and refurbishment |
| Nozzle inserts and bushings | New manufacture and replacement |
| Cutting-face hardfacing | New application and re-application |
| Heating and insulation assembly | New manufacture and replacement |
| Matched die and knife set | New manufacture and regrind |
Die plates are supplied individually, as a matched die and knife set, or within a wider extruder and pelletizer package covering shafts, screws and screw elements, barrels, pelletizer knives, mechanical seals, couplings and bearing bushes — including Nordson BKG Type AH D drive and rotor parts — with interface dimensions coordinated across the assembly.
| Application | Materials |
|---|---|
| Die body | Hot-work and nitriding tool steels (H13, 1.2344; 31CrMoV9) and stainless grades for corrosive compounds; hardened and stress relieved |
| Cutting face | Stellite and tungsten carbide hardfacing, HVOF carbide coatings, brazed carbide rings |
| Nozzle inserts | Tungsten carbide, ceramic and hardened tool steel, selected to the compound and pellet size |
| Insulation and heating | Thermal insulation plates and pressure-tight heater bodies to original specification |
Cutting-face and nozzle materials are matched to the compound — abrasive, filled, glass-reinforced or corrosive — and upgraded where the original was under-specified.
In most cases the cutting face can be restored to original flatness and the nozzles returned to original bore at a fraction of the cost of a new plate.
Die plates resurfaced with an upgraded cutting-face material routinely outlast the original.
We hold the technical information needed to produce die plates for the platforms above. Where a plate is obsolete, undocumented or from an out-of-production machine, we reverse engineer it from a sample plate or from the mating cutter and cutting chamber: nozzle pattern, hole count, bore and land length, face flatness and finish, bolt circle, heating and insulation layout and cutting-face material. The resulting manufacturing drawing package becomes the permanent record for repeat supply.
Every die plate is delivered with material certificates, hardness and dimensional inspection records, nozzle-by-nozzle bore and flatness reports, pressure test records for the heating circuits, and a die-face-to-knife contact check for matched sets. Manufacturing is carried out at ISO 9001 certified facilities.
2570 N. First Street, Second Floor, San Jose, CA 95131, USA
Tel. +1-408-892-2364