- Home
- Extruders and Pelletizers
- Pelletizer Knives
Pelletizer Knives
Cutter blades, blade holders and cutter hubs — new manufacture and regrind
Cutter blades, blade holders and cutter hubs — new manufacture and regrind
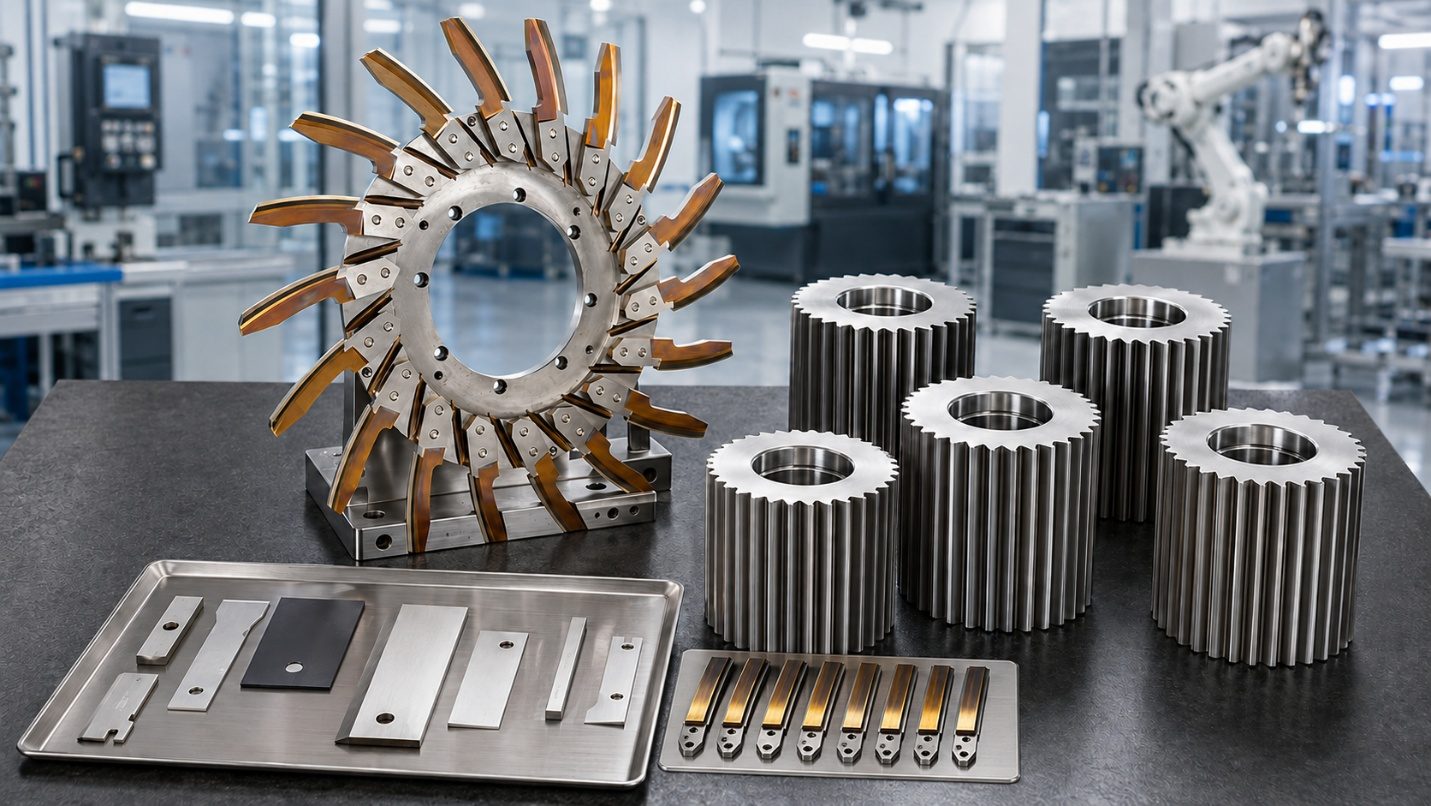
We manufacture pelletizer knives, cutter hubs and blade holders for the pelletizer heads attached to extruders, and regrind worn knives to original profile. Blades are supplied in tool steel, martensitic stainless, hardfaced and carbide-tipped grades, cut to your die face geometry, cutting angle and blade pressure, and matched as a set.
Underwater pelletizer knives — die-face cutting blades in matched sets, profiled to the die plate cutting face, hub diameter and blade count of your machine.
Water-ring and hot-face knives — die-face blades for water-ring, air-cooled and hot-face systems, with the relief and contact geometry of the original.
Strand pelletizer knives — helical and straight rotor blades and fixed bed knives, ground as matched pairs for correct shear and pellet length.
Cutter hubs and blade holders — hubs, blade carriers, clamps and holders, balanced and machined to the cutter shaft fit and blade seating plane.
Carbide-tipped and hardfaced blades — tungsten carbide tipped and Stellite-faced edges for abrasive, filled and glass-reinforced compounds.
Blade fixing hardware — clamping screws, blade clamps, shims, spacers, spring and pressure elements for blade load adjustment.
Regrind service — worn knives reground to original profile, cutting angle and blade height, and returned as a set matched within tolerance so blade load is even across the die face.
We manufacture, supply and regrind knives, cutter hubs and blade holders for all extruder and pelletizer platforms in service today, including — but not limited to — the machines below.
| Manufacturer | Extruder and pelletizer models and families |
|---|---|
| JSW — The Japan Steel Works | CMP251, CMP274, CMP308, CMP335, CMP362, CMP387, CMP443; CIM360, CIM400, CIM460, CIM510, CIM560 |
| Kobelco | LCM, KTX and TSR families; LCM-H, LCM-EX, LCM-G, Hyper KTX, NEX-T, Mixtrumat and NCM legacy families |
| Coperion | ZSK MEGAcompounder family, including ZSK 380 and ZSK 420 |
| ENTEK | HT 162 |
| Farrel Pomini | FCM and FMP systems, including FMP100 |
| KraussMaffei | KE, ZE-PC and ZE BluePower families |
| Leistritz | ZSE 260 MAXX |
| Pelletizing systems | Nordson BKG, including Type AH D drive and rotor parts; Gala, Maag and equivalent underwater, water-ring and strand pelletizing systems |
| All other makes | Knives, hubs and blade holders for the pelletizer heads of single-screw, co-rotating and counter-rotating twin-screw extruders, of any manufacturer, model or age |
Platforms not listed are equally within scope, including obsolete and out-of-production equipment reproduced by reverse engineering. The extruder manufacturer and model are sufficient to open a project.
Our extruder program is built around JSW equipment. We hold established manufacturing experience across the CMP and CIM platforms: die face and blade contact geometry, cutting angle and relief, hub diameter, blade count and seating planes, blade load arrangements, edge material specifications and the wear mechanisms that limit knife life on these machines.
The following components are supplied for the JSW CMP251, CMP274, CMP308, CMP335, CMP362, CMP387 and CMP443, and for the CIM360, CIM400, CIM460, CIM510 and CIM560:
| Component | Supply |
|---|---|
| Underwater pelletizer knives | New manufacture and regrind |
| Water-ring, hot-face and strand knives | New manufacture and regrind |
| Cutter hubs and blade holders | New manufacture and refurbishment |
| Carbide-tipped and hardfaced blades | New manufacture and re-tipping |
| Blade fixing hardware and shims | New manufacture and replacement |
| Matched die and knife set | New manufacture and regrind |
Knives are supplied individually, as a matched set with the cutter hub and die plate, or within a wider extruder and pelletizer package covering shafts, screws and screw elements, barrels, die plates, mechanical seals, couplings and bearing bushes — including Nordson BKG Type AH D drive and rotor parts — with interface dimensions coordinated across the assembly.
| Application | Materials |
|---|---|
| Blades — general compounding | 1.2379 / D2, M2 and equivalent tool steels, heat treated to the working hardness of the original |
| Blades — wet and corrosive service | 420 and 440C martensitic stainless steels |
| Blades — abrasive and filled compounds | Tungsten carbide tipped and Stellite hardfaced edges; PM tool steels |
| Cutter hubs and holders | Alloy and stainless steels, hardened where the blade seats, dynamically balanced |
Edge material and hardness are matched to the compound and the die-face material, and upgraded where the original was under-specified.
In most cases the edge can be reground to original profile and the set returned to service several times over, at a fraction of the cost of a new blade set.
A knife set matched within tolerance cuts evenly across the die face; one blade standing proud takes the load, raises die-face temperature and starts tails, doubles and freeze-off.
We hold the technical information needed to produce knives for the platforms above. Where a knife is obsolete, undocumented or from an out-of-production machine, we reverse engineer it from a sample blade or from the mating cutter hub and die plate: blade length, width and thickness, cutting angle and relief, edge profile and radius, blade height above the hub, mounting hole pattern and clamping geometry, material and hardness. The resulting manufacturing drawing package becomes the permanent record for repeat supply.
Every knife set is delivered with material certificates, hardness records, blade height and profile inspection reports, set-matching records, hub balancing records where applicable, and a die-face contact check for matched sets. Manufacturing is carried out at ISO 9001 certified facilities.
2570 N. First Street, Second Floor, San Jose, CA 95131, USA
Tel. +1-408-892-2364